Terjemahan

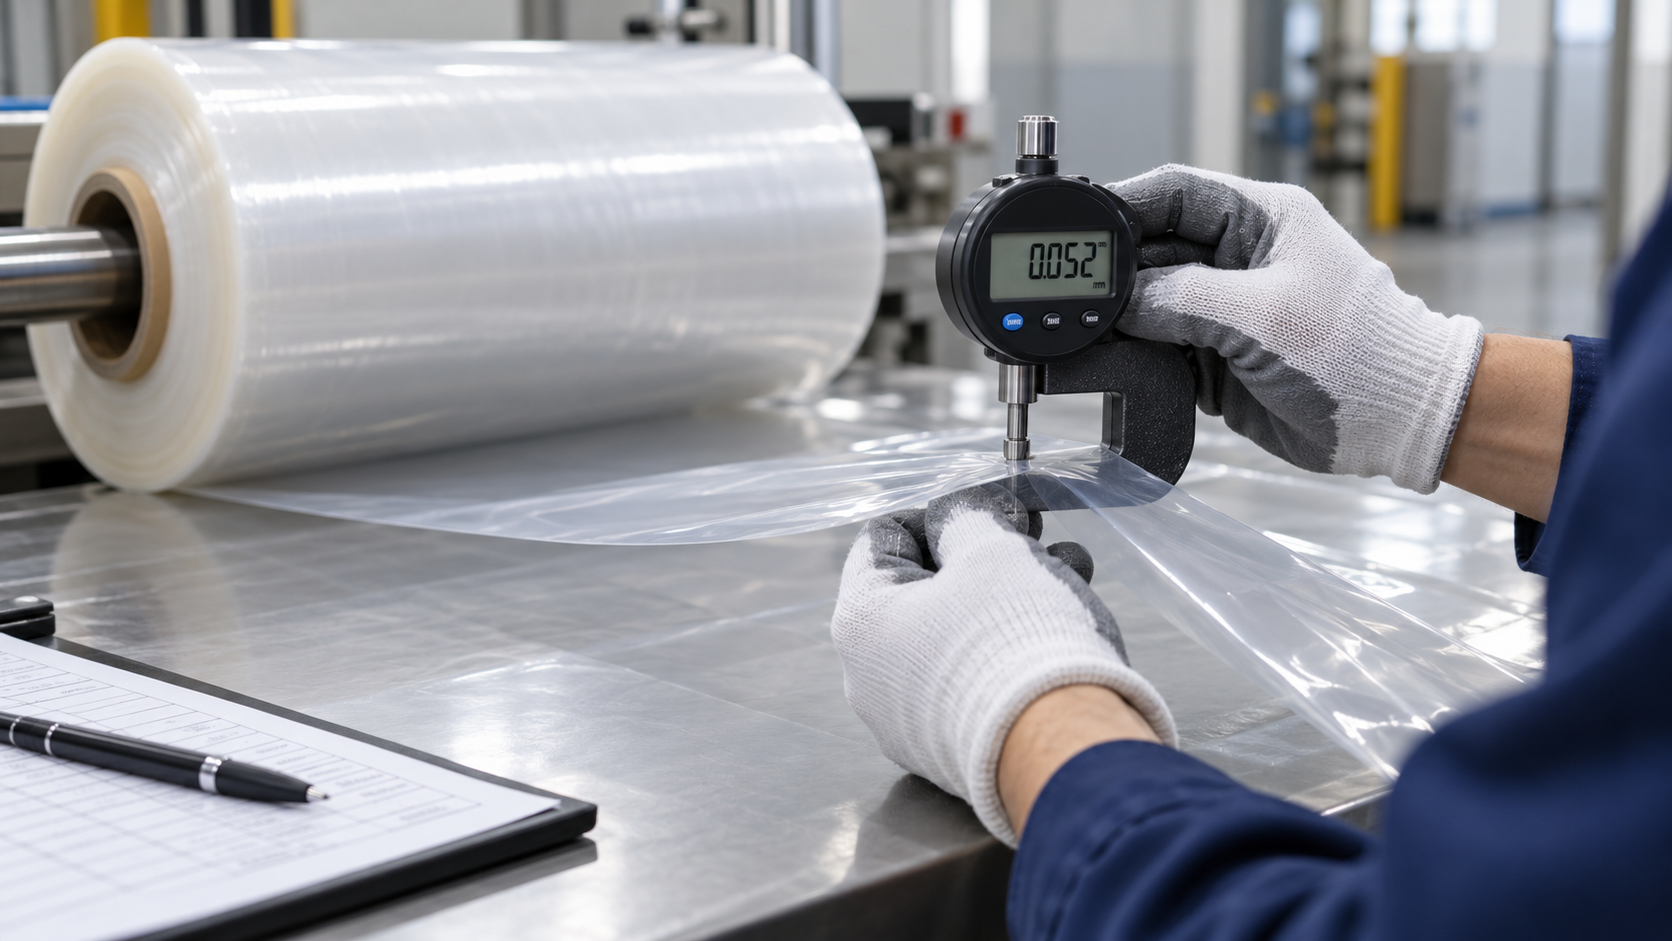
Buyers sometimes measure PE film at several locations and find that the readings are not identical to the nominal number on the purchase order. A film specified as 50 microns, for example, may show small variations from one point to another.
This does not automatically mean the material is defective. In blown film extrusion, nominal micron is a target gauge, and some degree of PE film thickness variation must be managed through an agreed tolerance, measurement method, and sampling plan.
Why Can Film Thickness Vary?
Blown film is produced by melting resin, passing the polymer through a circular die, expanding the tube into a bubble, cooling it, and drawing it upward.
Throughout this continuous process, melt flow and bubble conditions must remain balanced. Small changes in several variables can influence the finished gauge profile.
1. Melt Distribution Through the Die
The polymer melt should exit relatively evenly around the annular die.
Die-gap conditions, temperature differences, contamination, or uneven flow can cause one region to become slightly thicker or thinner. As the bubble travels and is eventually collapsed into lay-flat film, this variation can appear as a repeating profile across the roll.
2. Bubble Stability and Blow-Up Ratio
Air inside the bubble controls its diameter. Changes in bubble diameter or instability during production can affect film width and gauge distribution.
Blow-up ratio, extruder output, and haul-off speed all interact to establish final thickness. Stable bubble control is therefore an important part of maintaining consistent gauge.
3. Uneven Cooling
An air ring cools the molten bubble after it exits the die.
If airflow is not balanced, one section can cool faster than another. This can affect bubble behavior, frost-line position, and the thickness profile around the film.
4. Resin and Formulation Changes
Changing resin grade, blend composition, additives, melt index, or density can alter processing behavior.
A machine that runs steadily with one formulation may require adjustments when the material composition changes. Raw-material control and processing conditions therefore need to be managed together.
Nominal Thickness vs Average Thickness
Buyers should distinguish between several concepts:
- Nominal thickness: the target gauge in the specification.
- Individual reading: one measurement at a specific location.
- Average thickness: the average of several measurements.
- Thickness profile: the pattern of gauge variation across or along the film.
ASTM D8136 is specifically designed to characterize plastic film thickness and thickness variability in both transverse and machine directions for quality control, process support, inspection, and buyer-seller communication.
Why Can One Measurement Be Misleading?
One gauge reading cannot reliably describe an entire roll.
If the measurement happens to fall at the thinnest or thickest point in the profile, it may not represent the average material. Inspection should therefore follow a defined sampling plan with multiple points across the width and, where necessary, at multiple positions along the roll.
Measurement method also matters. ASTM D8136 notes that results from different thickness-measurement procedures should not automatically be expected to agree exactly.
How Should Buyers Specify Thickness Tolerance?
There is no universal PE film tolerance that is correct for every product. The acceptable range depends on process capability, application risk, nominal thickness, and measurement method.
A stronger purchase specification does not only state:
“Thickness: 60 microns”
It can also define:
- Nominal thickness
- Agreed tolerance
- Whether tolerance applies to individual readings or an average
- Measurement method
- Number and location of samples
This gives the customer and supplier the same basis for acceptance.
Is a Tighter Tolerance Always Better?
Not necessarily.
An unnecessarily tight tolerance can increase reject rates or require additional process control without providing a meaningful application benefit. A tolerance that is too wide, however, can allow local thin spots that increase puncture, tear, or weight-consistency risk.
The specification should therefore be based on packaging function rather than an arbitrary number.
How Does Thickness Variation Affect Bag Weight?
Gauge variation also affects finished bag weight. Because theoretical weight is based on area × thickness × density, changes in average gauge affect kilograms per thousand bags and pieces per kilogram.
For this reason, buyers should evaluate gauge and finished-product weight together when reviewing quotations or incoming material.
Related Reading
- What Does Micron Mean in Plastic Film? A Buyer’s Thickness Guide
- PE Film Thickness Guide by Application
- Product Specification
Conclusion
PE film thickness is not perfectly identical at every point because blown film is a continuous process influenced by the die, bubble, cooling, resin formulation, and line conditions.
Buyers should clearly define nominal thickness, tolerance, sampling, and measurement method so that inspection is based on an agreed standard.
For the fundamentals of gauge specification, see Dynaplast's micron thickness guide. PT Dynaplast Mandiri monitors film thickness and dimensional accuracy as part of production quality control.